In today’s fast-paced construction and mining industries, efficiency and cost control are paramount. As companies look for innovative ways to maximize productivity while reducing operational costs, mobile crushers are quickly becoming the go-to solution for many. Specifically, crawler mobile crushers offer unparalleled flexibility and cost-effectiveness, making them a game-changer for stone and aggregate processing.
I. Flexibility at Its Best
One of the primary advantages of mobile crushers, particularly the crawler mobile models, is their mobility. Traditional crushing plants are fixed in place, often requiring significant transportation and installation costs when new sites are needed. However, mobile crushers are designed to move directly to the job site, reducing transportation costs and downtime. Their ability to adapt to different work environments and work alongside other machinery also ensures smooth operations and increased efficiency.
II. Cost-Effective Crushing Solutions
Mobile crushers not only offer flexibility, but they also significantly reduce operational costs. By eliminating the need for transporting large amounts of raw materials to stationary plants, companies can cut down on fuel, labor, and logistics costs. The integrated design of mobile crushing stations allows for the direct processing of raw materials on-site, minimizing waste and maximizing material output. This on-site processing capability helps businesses save on long-distance transportation and processing time, resulting in more cost-effective operations.
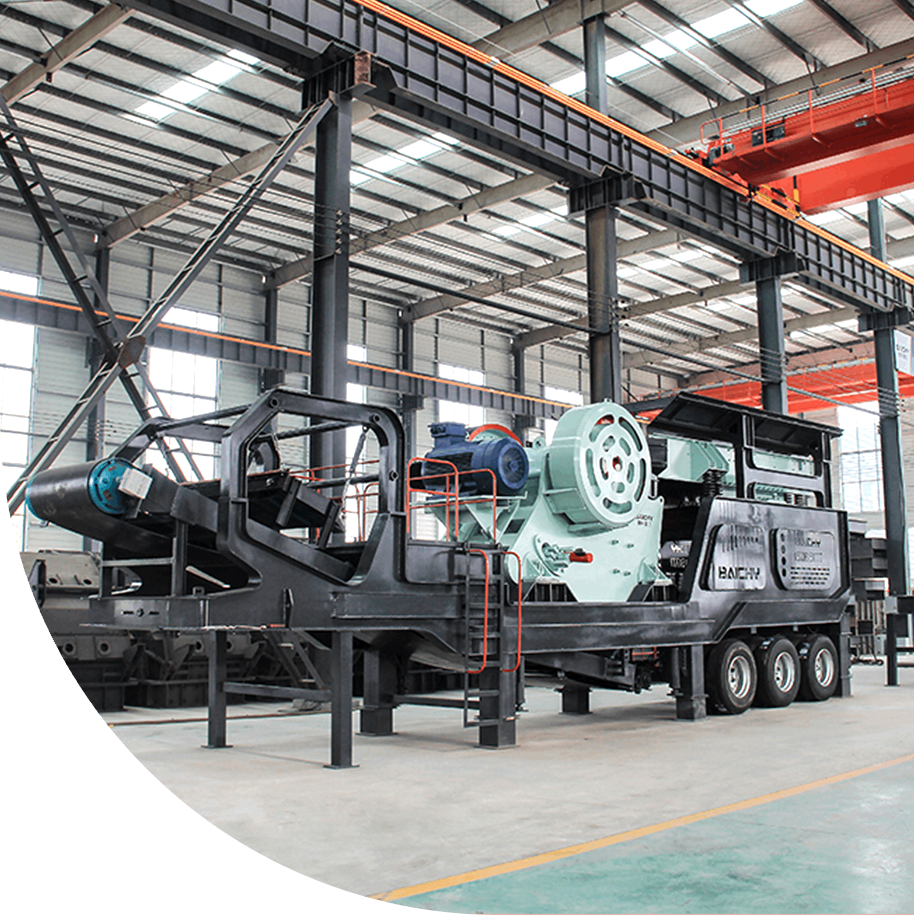
Granite resources are widely distributed around the world and have become an important source of high-quality aggregates for infrastructure construction. High-speed railways, highways, bridges, ports, and urban development projects require large quantities of durable crushed stone materials.However, granite has high hardness, dense structure, and strong wear resistance, which creates higher requirements for crushing equipment. Ordinary crushing machines may experience rapid wear, unstable output, and increased maintenance costs when processing granite continuously.The 200TPH tire-mounted crushing station is designed to meet these challenges. By combining powerful crushing equipment with a flexible mobile structure, it provides mining enterprises with a reliable solution for continuous granite aggregate production.
I. How Does a 200TPH Tire-Mounted Crushing Station Work in Granite Mining Operations?
At the mining site, large granite rocks extracted from the quarry are first transported to the vibrating feeder. The feeder evenly delivers raw materials into the primary jaw crusher for initial crushing.The heavy-duty jaw crusher applies strong compression force to break large granite blocks into smaller sizes. After primary crushing, the materials are transported to the secondary crushing stage, where cone crushers or impact crushers further reduce particle size and improve aggregate shape.The processed materials then enter the vibrating screening system for classification. Different sizes of finished granite aggregates are separated and transported by conveyors for storage or direct use in construction projects.
II. How Does the Mobile Crushing Station Handle Hard and Abrasive Granite?
Granite is one of the typical hard rocks with high compressive strength and strong abrasiveness. Efficient granite processing requires equipment with durable structures and excellent wear resistance.The 200TPH tire-mounted crushing station adopts heavy-duty crushing components and optimized equipment configuration to maintain stable performance under demanding mining conditions. The jaw crusher provides powerful primary crushing capability, while the secondary crushing equipment improves particle shape and product quality.The combination of reliable crushers, durable wear parts, and reasonable process design helps extend equipment service life and reduce unexpected downtime during long-term granite production.
| Parameter |
Value / Description |
| Equipment Name |
Mobile Crushing Station |
| Equipment Type |
Wheel / Crawler Mounted Mobile Crushing Plant |
| Main Applications |
Mining, Quarrying, Construction Waste Recycling, Highway & Railway Aggregate Production |
| Processed Materials |
Granite, basalt, limestone, iron ore, construction waste and other stones & ores |
| Working Environment |
Open pit quarry, construction site, urban solid waste treatment site |
| Mobility Advantage |
No need for fixed foundation, quick site relocation |
| Key Advantages |
Strong mobility, save transportation cost, compact layout, flexible configuration, adapt to complex site |
III. How Does the Tire-Mounted Design Improve Granite Quarry Production Flexibility?
Traditional fixed crushing plants usually require large foundations and long installation periods, which may limit production flexibility. For mining projects where extraction locations change frequently, mobile crushing equipment provides significant advantages.The tire-mounted design allows the 200TPH crushing station to be transported easily between different working areas. When mining progresses to a new location, the equipment can be relocated quickly without rebuilding the entire production system.This mobility enables operators to process granite closer to the quarry face, reducing truck transportation distance and improving overall project efficiency.
IV. Versatile Applications Across Industries
Mobile crushers are not limited to just one type of job; they are versatile machines that can handle a variety of applications. Whether it’s construction, mining, or quarrying, crawler mobile crushers can process a range of materials, including rocks, stones, and aggregates, making them invaluable in multiple sectors. From large-scale mining projects to smaller construction jobs, the ability to quickly move and set up crushing operations on-site is a huge advantage.
V. A Sustainable Future for Crushing Operations
The growing emphasis on sustainability in the construction and mining industries makes mobile crushers even more relevant. With their ability to operate efficiently in diverse environments while reducing energy consumption and waste, mobile crushers align with eco-friendly initiatives. Their minimal environmental impact, coupled with their ability to reduce the carbon footprint associated with transportation, makes them an attractive option for companies committed to sustainable practices.
As the demand for more efficient and cost-effective solutions continues to rise in the construction and mining industries,
mobile crushers are proving their worth. Offering flexibility, reducing costs, increasing productivity, and supporting sustainability, these machines are essential tools for businesses seeking to stay competitive in today’s fast-evolving markets. With mobile crushers, companies can ensure they are meeting the demands of the future while improving their bottom line.
Q: What are the main factors to consider when selecting primary crushing equipment?
A: Key considerations include: material hardness and abrasiveness, required capacity, feed size, product size requirements, and mobility needs. Our technical team can help analyze your specific conditions to recommend the optimal solution.
Q: How does your mobile crushing plant compare to stationary plants in terms of cost-effectiveness?
A: Mobile plants offer significant advantages in reduced infrastructure costs and flexibility, making them ideal for multiple sites or temporary projects. However, for large-scale, long-term operations, stationary plants may provide better economy of scale.
Q: What maintenance routines do you recommend for ensuring optimal crusher performance?
A: We recommend: daily inspections of wear parts, regular lubrication according to our manual, monitoring of operating parameters, and scheduled replacement of consumables based on actual operating conditions.
Q: Can your equipment handle varying material hardness within the same operation?
A: Yes, our modern crushing equipment features hydraulic adjustment systems and automatic control functions that can adapt to material hardness variations while maintaining consistent product quality.
Q: What after-sales support and technical training do you provide?
A: We offer comprehensive support including: installation supervision, operator training, maintenance guidance, readily available spare parts, and remote technical assistance to ensure optimal equipment performance.